How to Choose a CNC Tube Bending Machine for Automotive and Exhaust Production
News 2026-09-04
Automotive and exhaust components look simple until they reach the bending department. A single part may contain several bends on different planes, short distances between bends, tight radii, and strict requirements for fit-up. If the bend angle, rotation, or length between bends changes from one piece to the next, the problem quickly appears during welding and final assembly. Choosing the right CNC tube bending machine is therefore not only a machine-purchasing decision. It is a decision about process stability, labor, tooling, quality control, and the future range of parts a factory can accept.
This guide explains the information an automotive or exhaust manufacturer should prepare before requesting a quotation. It also shows how to compare machine configurations without relying only on maximum tube diameter or motor power.
Start With the Finished Part, Not the Machine Catalogue
The best starting point is a complete drawing of the bent part. The drawing should identify the tube outside diameter, wall thickness, material grade, centerline radius, bend angles, straight lengths, and rotation between bends. If a formal drawing is not available, a physical sample and a clear dimension sheet can help the machine supplier understand the application.
A machine described as suitable for a certain maximum diameter may still be unsuitable for a particular component. A 60 mm thin-wall mild-steel exhaust tube and a 60 mm thick-wall stainless-steel structural tube create very different loads. Bend radius and material strength matter as much as diameter. For this reason, experienced suppliers review the full combination of material, diameter, wall thickness, radius, and geometry before confirming a model.
Define the Material and Tube Specification
Automotive and exhaust production commonly uses carbon steel, stainless steel, aluminized steel, and aluminum. Each material has its own springback, surface behavior, and forming limits. Stainless steel normally requires more force than mild steel and may show greater springback. Aluminum can mark easily and may need carefully prepared tooling surfaces. Welded tube can also behave differently depending on weld-seam position and consistency.
Send the actual material standard to the supplier instead of saying only “steel” or “stainless steel.” Include the following details:
- Outside diameter and manufacturing tolerance
- Nominal and minimum wall thickness
- Material grade and tensile properties when available
- Welded or seamless tube construction
- Required surface finish and acceptable marking
- Tube length before bending
Suzhou Jiuqiang Machinery Technology Co., Ltd. supplies solutions for iron, stainless-steel, aluminum, copper, aluminum-profile, and other metal-tube applications. Depending on the material and machine configuration, solutions can be evaluated for tube sizes up to 114 mm in outside diameter and wall thicknesses up to 10 mm. Final capacity must always be confirmed against the real part and material.
Understand Centerline Radius and Bending Difficulty
The centerline radius, often abbreviated as CLR, is one of the most important values in tube bending. A generous radius is normally easier to produce than a tight radius. As the ratio between the centerline radius and tube diameter becomes smaller, the risk of outside-wall thinning, inside-wall wrinkling, ovality, and cracking increases.
Exhaust systems often require compact bends so that the assembly fits within limited vehicle space. These parts may need a mandrel inside the tube and a wiper die near the tangent point. The mandrel supports the tube cross-section, while the wiper die helps control material on the inside of the bend. The exact tooling arrangement depends on the radius, wall factor, material, and acceptable ovality.
Do not assume that a mandrel automatically solves every defect. Correct tool design, pressure-die setting, clamp length, lubrication, tube consistency, and machine rigidity all work together. A sample bend trial using production material is far more useful than a general statement that the machine “can bend” the listed diameter.
Compare CNC Axes and Automation Functions
A CNC tube bending machine typically controls feeding, tube rotation, and bending. Additional controlled functions may improve flexibility or reduce setup time. When comparing quotations, ask which movements are servo controlled and which adjustments remain hydraulic or manual.
For parts with multiple bends on different planes, automatic feeding and rotation reduce operator measurement and positioning errors. The program stores the length, rotation, and angle for each bend. This is especially valuable when a factory produces right-hand and left-hand components, families of exhaust parts, or several vehicle models on the same line.
Automation should match production volume. A high-volume line may justify automatic loading, seam detection, piercing, cutting, unloading, or integration with inspection equipment. A job shop producing smaller batches may gain more from quick tooling changes, clear program management, and flexible part support. Adding every possible option increases cost and complexity without necessarily improving the business case.
Calculate Real Production Capacity
Catalogue bending speed does not equal finished-parts output. Total cycle time includes loading, clamping, feeding, rotating, bending, retracting the mandrel, unloading, and any operator handling. A long component may also need a support table or following device to avoid collision and uncontrolled movement.
Prepare an hourly or shift-based production target. Then ask the supplier to estimate cycle time using the actual number of bends and the proposed automation level. The calculation should include realistic handling time rather than only machine motion. If one operator will manage multiple machines, loading and unloading strategy becomes even more important.
For mixed production, changeover time deserves equal attention. A machine that produces one part very quickly but requires several hours for tooling and program change may not be the best choice for frequent small batches.
Specify Quality Requirements Clearly
“High accuracy” is not a measurable purchasing requirement. Define how the finished part will be inspected and which dimensions are critical. Common checks include bend angle, distance between bends, plane rotation, overall envelope, end position, ovality, outside-wall thinning, and surface appearance.
Springback compensation is essential for repeatable angles. CNC control makes corrections easier, but stable incoming tube material remains important. If tube hardness, wall thickness, or weld quality varies considerably, the finished parts will vary even when the machine repeats the same movement accurately.
Ask for sample parts and an inspection report before final acceptance when the application is demanding. Ideally, the trial uses the buyer’s production material. Photographs are useful for early evaluation, but measured samples provide much stronger evidence.
Evaluate Tooling as Part of the Complete System
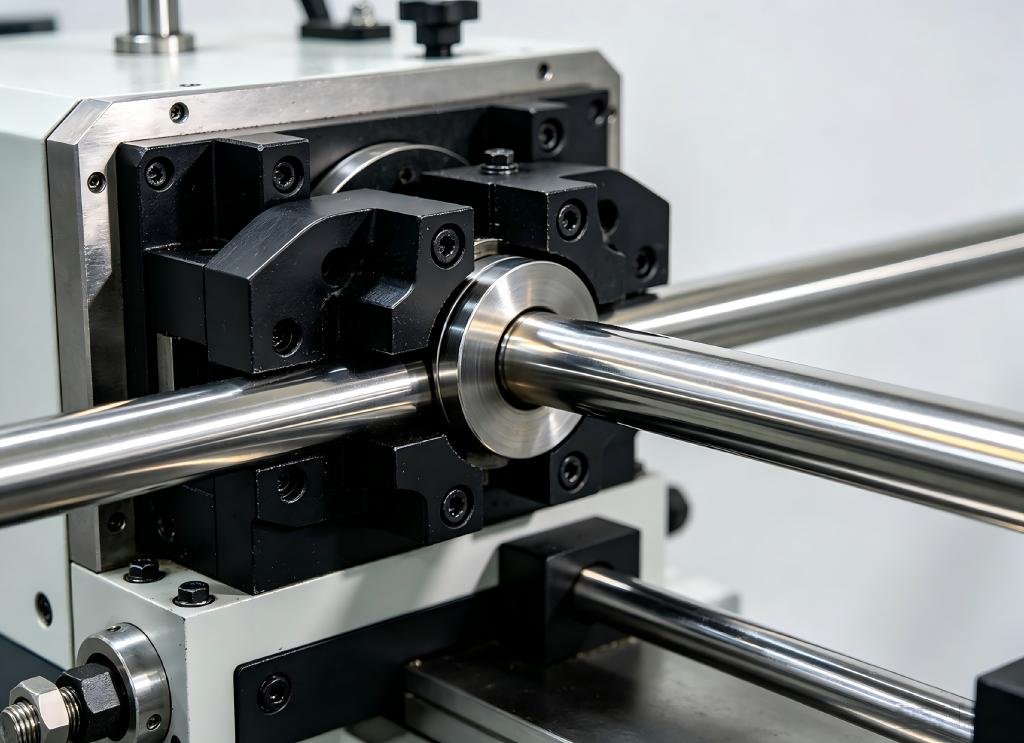
Bending tooling is not a minor accessory. It determines how the tube is held, supported, and formed. A rotary-draw bending set may include the bend die, clamp die, pressure die, mandrel, wiper die, and collet. Tool material, heat treatment, surface finish, and geometry should suit the tube material and expected production volume.
When reviewing a quotation, confirm how many tooling sets are included, which tube size and radius each set supports, and whether wear parts are available. If one product family uses several radii or diameters, list every combination. Tool storage and identification also matter in a factory with frequent changeovers.
Plan for Integration and Future Products
The machine should fit the current component, but a purchase normally serves several years of production. Review likely future tube diameters, materials, bend radii, and part lengths. Reasonable spare capacity can protect future flexibility, while excessive oversizing may reduce efficiency and increase tooling cost.
Also check factory layout, electrical supply, hydraulic requirements, air supply, operator access, material flow, and safety zones. For an integrated cell, define the communication interface and responsibility for loading equipment, robots, cutting machines, and inspection systems before the project begins.
Service, Training, and International Project Support
For buyers in Mexico, Spain, Argentina, and other export markets, service planning should be discussed before shipment. Ask what documents, electrical drawings, operation manuals, program backups, spare-parts lists, and remote-support methods are supplied. Operator and maintenance training should cover tooling installation, parameter adjustment, lubrication, daily inspection, fault diagnosis, and safe operation.
Language is another practical consideration. Clear English documentation, labeled electrical components, and structured remote diagnosis can shorten commissioning and recovery time. The buyer should also nominate responsible operators and maintenance staff early enough to participate in acceptance and training.
A Practical RFQ Checklist
Before requesting a CNC tube bender quotation, prepare:
- Two-dimensional or three-dimensional part drawings
- Tube material, diameter, wall thickness, and length
- Centerline radius and number of bends
- Required output per hour or per shift
- Dimensional, ovality, thinning, and surface requirements
- Current and planned product families
- Preferred loading and unloading method
- Factory voltage and frequency
- Required tooling, spare parts, training, and acceptance tests
Conclusion
The right CNC tube bending machine for automotive and exhaust production is the one that controls the complete process: material variation, part geometry, tooling, handling, inspection, and changeover. Comparing machines only by maximum diameter can hide important differences and create expensive problems after delivery.
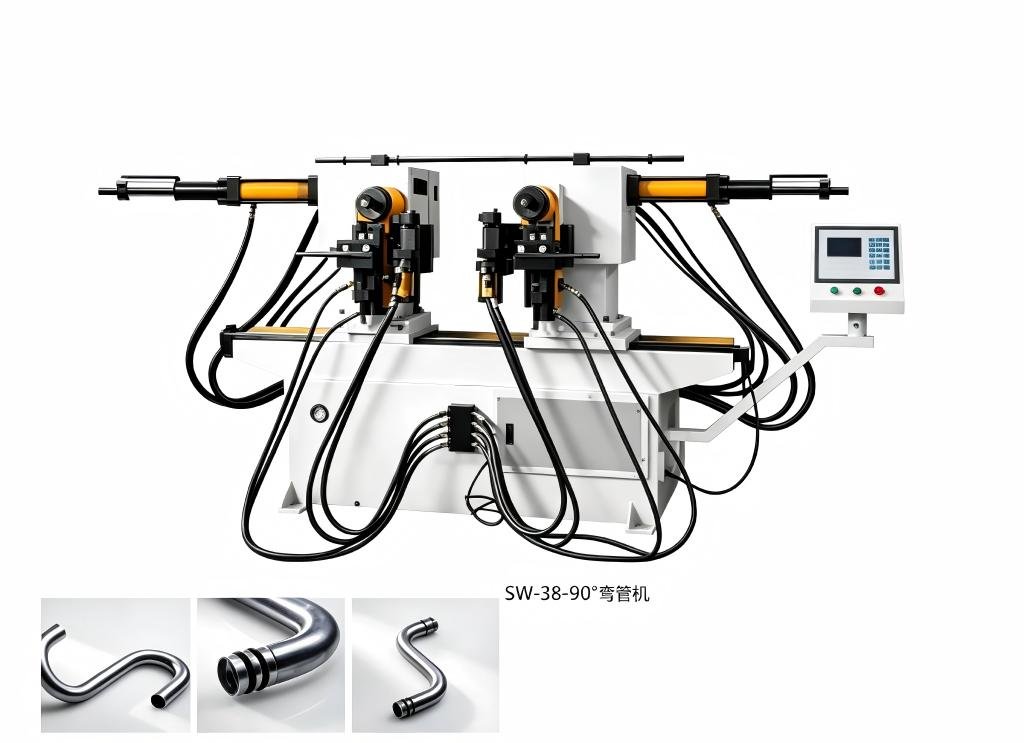
Suzhou Jiuqiang Machinery Technology Co., Ltd. provides CNC, hydraulic, fully automatic, and semi-automatic tube bending solutions for automotive, exhaust, furniture, shipbuilding, and other metal-processing industries. To receive a configuration proposal, send the part drawing, tube specification, required output, and quality criteria. A detailed application review allows the engineering team to recommend a suitable machine, tooling package, and automation level.